Automation
Plate Holder Welding Automation
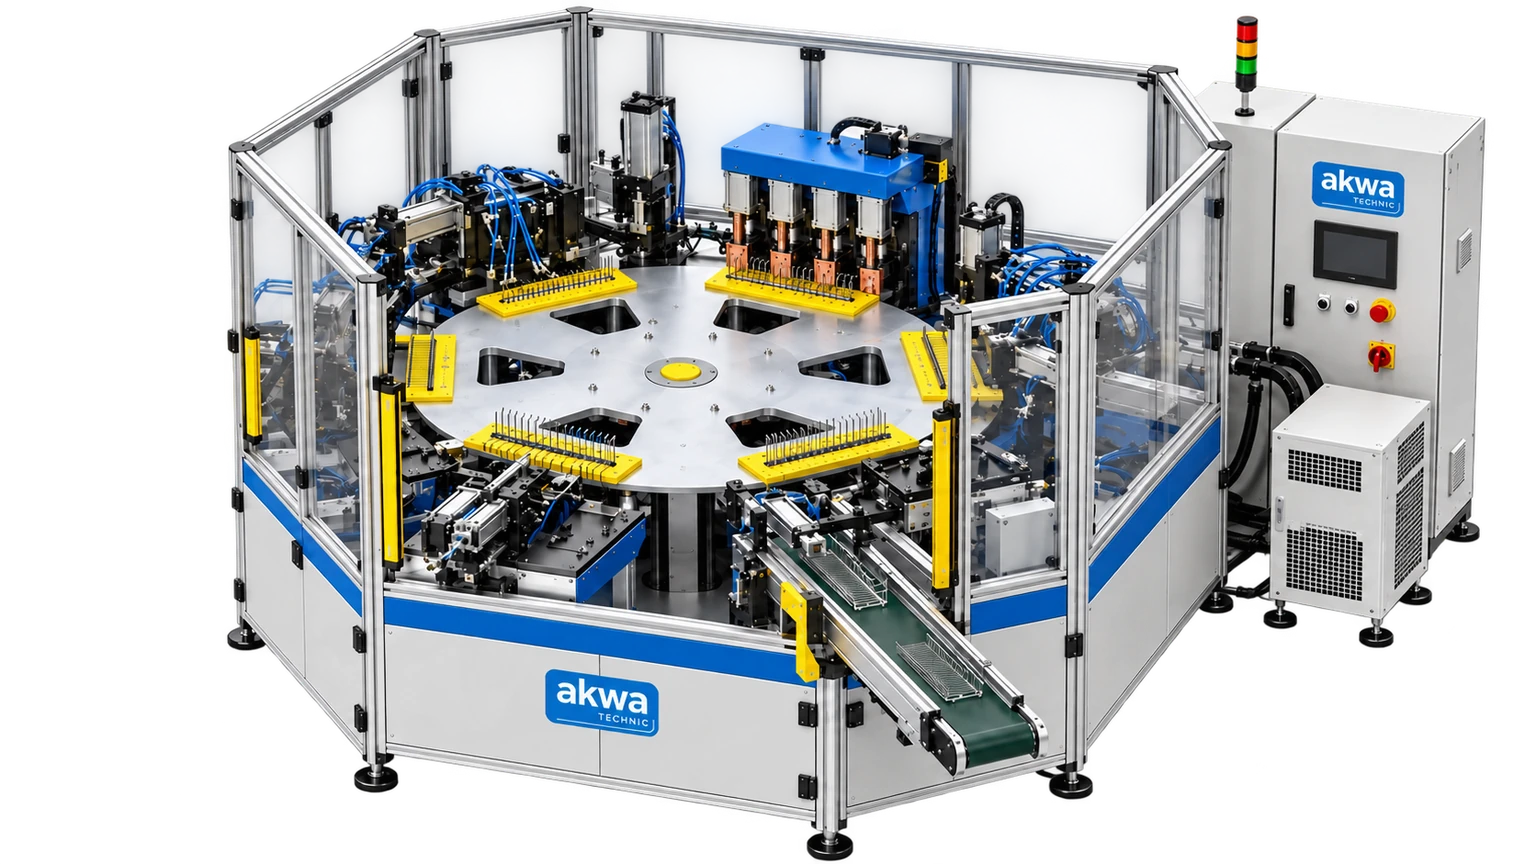
AKWA Technic Plate Holder Welding Automation combines loading, positioning and welding of backbone and pin wires with automatic transfer of finished parts to the output in one production cell. Both types have a 4-second cycle time. The 6-station type with servo-controlled ear bending and the 4-station type without bending are available with 4 × 60 kVA AC or 4 × 111 kVA MFDC welding transformers.
Configurations vary by model and application.
Request a quote AC / MFDC · View technical sheetNeed help? +90 (212) 485 88 71
PRODUCTION CONFIGURATIONS
Configure your machine.
Choose between two station layouts and two welding technologies.
Configuration: 6 stations · AC
Technical values for the selected model
| Number of stations | 6 |
| Cycle time | 4 s |
| Ear bending | Servo-controlled |
| Number of transformers | 4 |
| Rated power per transformer | 60 kVA |
| Rated power duty cycle | 50% |
| Welding technology | Alternating current (AC) |
| Operating frequency | 50/60 Hz |
| Reference secondary voltage | 7,1 V |
| Cooling type | Water-cooled |
Technical values are transcribed from the supplied current product information.
AC / MFDC · Plate Holder Welding Automation
| AC / MFDC | 6 stations · AC | 6 stations · MFDC | 4 stations · AC | 4 stations · MFDC |
|---|---|---|---|---|
| Number of stations | 6 | 6 | 4 | 4 |
| Cycle time | 4 s | 4 s | 4 s | 4 s |
| Ear bending | Servo-controlled | Servo-controlled | None | None |
| Number of transformers | 4 | 4 | 4 | 4 |
| Rated power per transformer | 60 kVA | 111 kVA | 60 kVA | 111 kVA |
| Rated power duty cycle | 50% | 20% | 50% | 20% |
| Welding technology | Alternating current (AC) | Medium-frequency direct current (MFDC) | Alternating current (AC) | Medium-frequency direct current (MFDC) |
| Operating frequency | 50/60 Hz | 1000 Hz | 50/60 Hz | 1000 Hz |
| Reference secondary voltage | 7,1 V | 8,3 V | 7,1 V | 8,3 V |
| Cooling type | Water-cooled | Water-cooled | Water-cooled | Water-cooled |
6-station type: Welding and servo-controlled ear bending
The backbone wires forming the plate holder’s supporting structure are loaded into the fixture. Guides and clamps hold them in the correct position throughout processing.
The pin wires supporting the plates are transferred to a comb fixture at spacings matching the product geometry.
Wire position and part presence are checked. The wires are centered and clamped ready for welding.
The joints between pin and backbone wires are welded by a four-transformer welding group. AC or MFDC technology is selected to suit production needs.
The plate holder ears are formed by a servo-controlled bending mechanism, completing ear bending within the welding automation.
The completed plate holder is removed from the fixture and transferred to the output conveyor. The rotary table prepares for the next cycle.
4-station type: Welding automation without bending
The backbone wires forming the plate holder’s supporting structure are loaded into the fixture. Guides and clamps hold them in the correct position throughout processing.
Pin wires are transferred to the comb fixture; wire arrangement and position are checked before welding.
The joints between pin and backbone wires are welded by a four-transformer welding group. AC or MFDC technology is selected to suit production needs.
The completed plate holder is removed from the fixture and transferred to the output conveyor. The rotary table prepares for the next cycle.
BUILT AROUND YOUR APPLICATION
Precision in every detail.
Family specifications from the current Akwa Technic catalog. The original technical sheet includes model-level ratings, dimensions, equipment and operating requirements.
| Cycle time | 4 s |
| Number of stations | 6 / 4 |
| Rated power per transformer | AC: 60 kVA (%50 DT) / MFDC: 111 kVA (%20 DT) |
Product features
- 6-station type: Welding and servo-controlled ear bending - 1. Backbone wire loading: The backbone wires forming the plate holder’s supporting structure are loaded into the fixture. Guides and clamps hold them in the correct position throughout processing.
- 6-station type: Welding and servo-controlled ear bending - 2. Pin wire loading: The pin wires supporting the plates are transferred to a comb fixture at spacings matching the product geometry.
- 6-station type: Welding and servo-controlled ear bending - 3. Centering and part inspection: Wire position and part presence are checked. The wires are centered and clamped ready for welding.
- 6-station type: Welding and servo-controlled ear bending - 4. Four-head resistance welding: The joints between pin and backbone wires are welded by a four-transformer welding group. AC or MFDC technology is selected to suit production needs.
- 6-station type: Welding and servo-controlled ear bending - 5. Servo-controlled ear bending: The plate holder ears are formed by a servo-controlled bending mechanism, completing ear bending within the welding automation.
- 6-station type: Welding and servo-controlled ear bending - 6. Automatic unloading: The completed plate holder is removed from the fixture and transferred to the output conveyor. The rotary table prepares for the next cycle.
- 4-station type: Welding automation without bending - 1. Backbone wire loading: The backbone wires forming the plate holder’s supporting structure are loaded into the fixture. Guides and clamps hold them in the correct position throughout processing.
- 4-station type: Welding automation without bending - 2. Pin wire loading and position inspection: Pin wires are transferred to the comb fixture; wire arrangement and position are checked before welding.
- 4-station type: Welding automation without bending - 3. Four-head resistance welding: The joints between pin and backbone wires are welded by a four-transformer welding group. AC or MFDC technology is selected to suit production needs.
- 4-station type: Welding automation without bending - 4. Automatic unloading: The completed plate holder is removed from the fixture and transferred to the output conveyor. The rotary table prepares for the next cycle.